

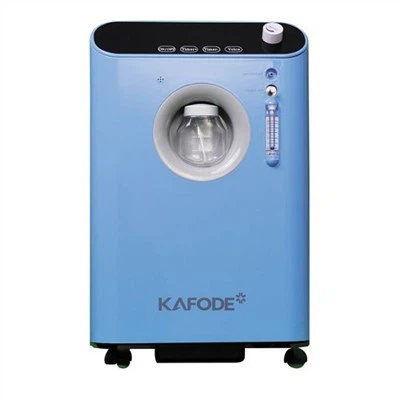
Stationary Oxygen Concentrator
Your Professional Stationary Oxygen Concentrator Supplier
We supply stationary oxygen concentrators for homecare, respiratory care, clinics, healthcare distributors, and medical equipment brands. Our current product range includes continuous-flow oxygen concentrators in configurations such as 5 LPM and 10 LPM, with specifications engineered for diverse clinical and homecare markets.
The product range is powered by pressure swing adsorption technology, utilizing ambient air as the feed gas and molecular sieve adsorption to separate nitrogen and deliver continuous oxygen-enriched gas. Standard and customizable configurations include adjustable flow control, real-time oxygen concentration monitoring, digital operational displays, power-failure protection, high- and low-pressure alarms, low-flow alarms, and high-temperature safety circuits.




Technical Specifications and Model Selection Criteria
|
Technical Parameter |
Engineering Benchmark and Published Range |
Procurement Relevance |
|
Oxygen Flow Rate |
1 to 5 LPM and 1 to 10 LPM models |
Determines patient oxygen volume capability |
|
Oxygen Concentration |
90 percent or higher at max recommended flow |
Verifies medical-grade purity under load |
|
Outlet Pressure |
30 to 60 kPa |
Ensures stable downstream delivery through humidifiers and tubing |
|
Input Power and Electrical |
350 VA (220V / 50Hz baseline; custom options available) |
Must match destination regional power grid |
|
Acoustic Noise Level |
60 dB(A) or lower average |
Critical for residential homecare acceptance |
|
Operating Environment |
5 degrees C to 40 degrees C; relative humidity 75 percent or lower |
Defines regional climate suitability |
|
Physical Dimensions and Weight |
380 x 355 x 610 mm, approx. 21.3 kg |
Affects freight shipping, warehousing, and handling |
Pressure Swing Adsorption System
Our stationary units utilize ambient air separation instead of compressed gas cylinders, maintaining an uninterrupted medical oxygen supply through a continuous cyclical process:
Ambient Air -> Intake Filtration -> Air Compression -> Molecular Sieve Adsorption -> Nitrogen Separation -> Oxygen-Enriched Gas -> Pressure Regulation -> Patient Outlet
The internal architecture integrates heavy-duty intake filters, oil-free compressors, high-efficiency lithium molecular sieve columns, electronic switching valves, cooling systems, and microcomputer control boards. This robust internal arrangement ensures long service intervals and consistent batch performance for commercial distribution.
Target Applications and Channel Solutions
We support diverse commercial models within the global healthcare supply chain:
Homecare and DME Providers
Focused on reliable continuous operation, low operational noise (60 dB(A) or lower), intuitive patient controls, and low maintenance overhead.
Clinics and Outpatient Facilities
Prioritizing steady clinical flow capacity, continuous runtime endurance, and multi-parameter alarm systems.
Medical Equipment Distributors
Requiring stable volume supply, consistent product specifications, robust packaging, spare parts availability, and comprehensive commercial support.
OEM and Private Label Partners
Tailored for established brands seeking contract manufacturing with customized housing aesthetics, control panel layouts, brand labeling, specialized user documentation, and customized cartoning.
Safety and Monitoring Alarms
Reliable fault detection safeguards institutional users and patients. Depending on the selected model configuration, our units incorporate:
Power Failure Protection
Triggers audible and visual alerts upon grid interruption.
Pressure Monitoring
Continuous tracking of high- and low-pressure anomalies within the pneumatic circuit.
Oxygen Purity Tracking
Real-time sensor indication for low concentration levels (below normal purity threshold).
Flow and Temperature Safety
Low-flow alerts and automatic thermal shutdown to protect the compressor.
Certifications and Regulatory Compliance
Quality Management
Production facilities operate under ISO 9001 certified quality management standards, ensuring standardized assembly, traceability, and batch consistency.
Export Documentation
Complete technical files, test reports, electrical schematics, and user manuals are supplied to assist distributors with local registration requirements.
Electrical Safety
Designs accommodate regional electrical compliance standards regarding insulation, leakage current, and electromagnetic compatibility.
Product reliability is enforced through strict manufacturing protocols:
Component Screening: Critical parts-including compressors, molecular sieve granules, microprocessors, and sensors-undergo strict incoming inspection.
Pneumatic and Electrical Assembly: Clean-room and structured assembly lines execute precision tubing, wiring, and structural bonding.
Comprehensive Run-Testing: Every finished unit undergoes computerized functional testing to verify flow output, concentration purity, outlet pressure, electrical safety, acoustic levels, and alarm responsiveness.
Final Audit: Finished goods are audited for surface finish, accessory completeness, and packaging integrity prior to palletizing.

Packaging and Export Logistics
Stationary oxygen concentrators are packed to withstand long-distance maritime and air logistics.
Carton Specifications
Individual heavy-duty corrugated export cartons featuring shock-absorbing internal foam protection.
Container Optimization
Standardized dimensions designed for efficient container space utilization.
Customization
Customized shipping marks, multi-language manuals, and palletized options are available upon request.
Frequently Asked Questions
We're professional stationary oxygen concentrator manufacturers and suppliers in China in China, specialized in providing high quality products with low price. We warmly welcome you to buy cheap stationary oxygen concentrator made in China here from our factory.
lightweight portable oxygen concentrator, oxygen concentrator lcd display medical, portable oxygen concentrator air separation system